7 Safety Risks AI Can Detect Across a Manufacturing Plant
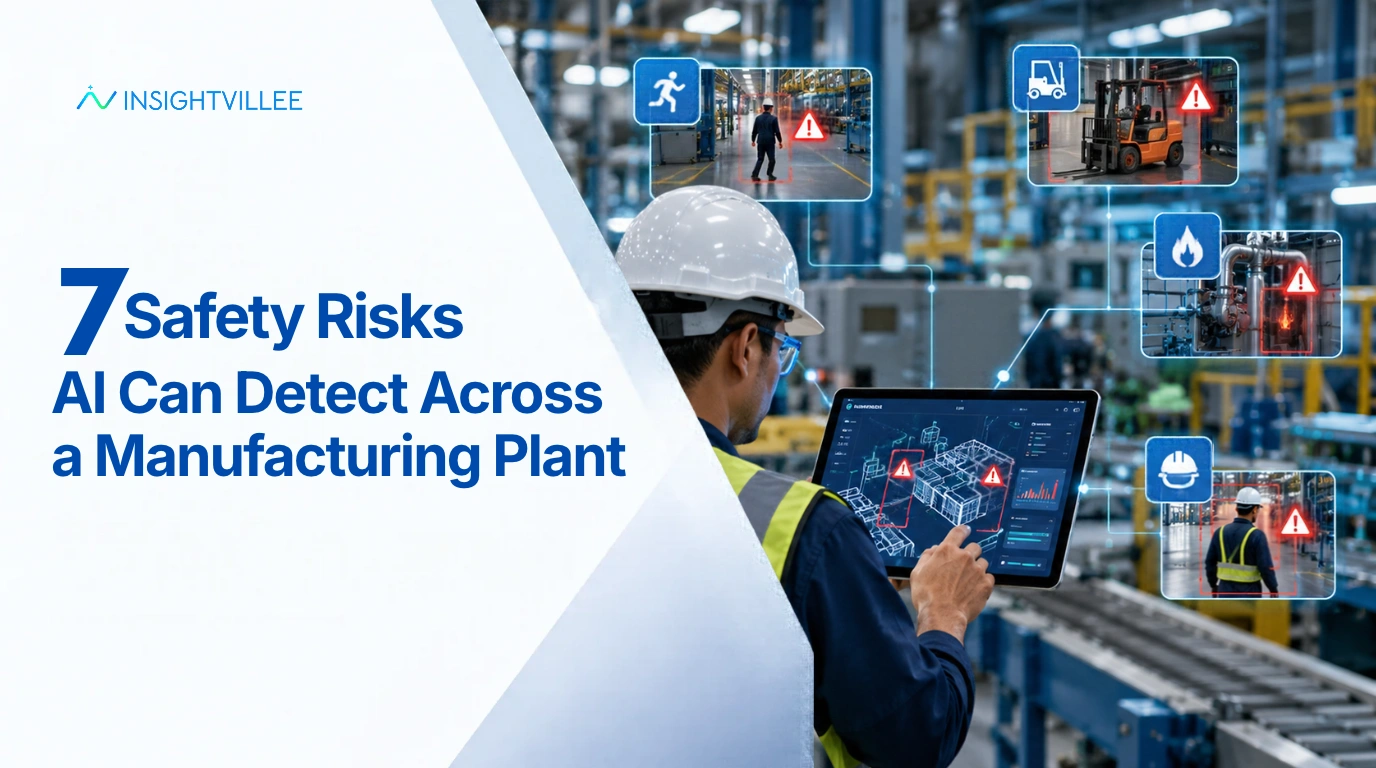
AI can help detect seven safety risks across manufacturing plants: missing protective equipment, restricted-area entry, unsafe machinery proximity, forklift-pedestrian interactions, slip and trip hazards, unsafe material storage, and visible smoke or fire.
AI Safety Monitoring uses appropriately configured cameras, sensors, and safety rules to identify these hazards and flag potentially dangerous conditions for investigation.
This helps manufacturers recognise workplace risks earlier, investigate recurring unsafe conditions, and take preventive action before incidents occur. Detection capabilities depend on the system and operating
environment.
Key Takeaways
- AI can detect seven manufacturing safety risks: PPE violations, restricted-area entry, unsafe machinery proximity, forklift hazards, slip and trip risks, unsafe material storage, and visible smoke or fire.
- Manufacturing hazards often go unnoticed because they occur between inspections or outside direct supervision.
- AI Safety Monitoring analyses camera and sensor data to identify predefined unsafe conditions and flag potential hazards.
- Recurring safety observations help identify high-risk areas, unsafe practices, and weaknesses in existing controls.
- Connected Industry 4.0 systems link safety information with production, equipment, and shift data for better investigations.
- AI-generated safety alerts require human verification before hazards or incidents are confirmed.
- AI safety monitoring complements physical safeguards, workplace inspections, worker reporting, and established safety procedures.
Why Do Manufacturing Safety Risks Go Unnoticed?
Manufacturing safety risks may remain unnoticed when hazardous conditions develop between inspections or occur outside normal supervision.
Large plants contain multiple production lines, warehouses, maintenance areas, and material-handling operations.
Safety teams cannot physically observe every activity at once.
Common visibility challenges include:
- Restricted areas receiving limited supervision
- Unsafe interactions occurring briefly
- Hazards developing between inspections
- Different risks across production areas
- Minor violations going unreported
Traditional inspections and worker reporting remain essential.
However, AI-supported monitoring can provide additional observations where suitable detection systems are deployed.
What Are the 7 Safety Risks AI Can Detect?
AI-based monitoring can help identify seven categories of visible manufacturing hazards, depending on camera coverage, available sensors, and detection capabilities.
| Safety risk | Potential AI detection |
| Missing PPE | Visible protective equipment violations |
| Restricted-area entry | People entering defined hazardous zones |
| Unsafe machinery proximity | Workers approaching dangerous equipment areas |
| Forklift-pedestrian risks | Unsafe vehicle and worker proximity |
| Slip, trip, and fall hazards | Visible spills, obstacles, or certain falls |
| Unsafe material storage | Blocked routes or visibly unsafe stacking |
| Smoke and fire | Visible smoke or flames |
These are potential applications of suitably configured AI safety systems, not features guaranteed by every manufacturing platform.
1. Missing or Improper PPE
Computer vision can identify certain visible PPE violations when the required protective equipment can be recognised reliably.
In manufacturing environments, workers may need:
- Safety helmets
- High-visibility jackets
- Protective eyewear
- Other task-specific equipment
An AI-enabled camera system may detect a worker without a required helmet or visible safety vest.
However, detection depends on camera angle, lighting, equipment visibility, and the models deployed.
Not all protective equipment can be assessed through images alone.
The purpose is to support PPE compliance checks, not replace supervisor inspections.
2. Entry Into Hazardous Areas
AI can identify people entering predefined restricted zones when those areas are covered by suitable cameras.
Examples include:
- Robot operating areas
- Restricted machinery zones
- Hazardous processing sections
- Automated material-handling areas
A camera-based system can compare detected worker positions against configured safety boundaries.
If someone enters a restricted area, it may flag the event for investigation.
However, camera monitoring does not replace physical guarding, interlocks, or access-control systems.
3. Unsafe Machinery Proximity
AI-supported monitoring may identify workers moving dangerously close to operating equipment or entering defined exclusion zones.
Potential concerns include:
- Workers approaching moving conveyors
- Unsafe access near robotic equipment
- Entry into machinery operating areas
- Unauthorised movement around automated systems
These situations may expose workers to moving machinery.
Detection requires accurate zone definitions and sufficient visibility.
Manufacturers should distinguish unsafe proximity from a confirmed near miss.
AI detection of near-miss events can help identify potentially dangerous interactions, but human verification is needed to determine whether an actual near miss occurred.
4. Forklift and Pedestrian Collision Risks
AI can support vehicle-pedestrian safety monitoring by identifying visible interactions and potentially unsafe proximity.
Forklifts operate near workers in warehouses, loading areas, and production facilities.
Potential risks include:
- Pedestrians entering vehicle routes
- Unsafe crossings
- Workers approaching reversing forklifts
- Vehicles operating near crowded work areas
Suitable monitoring systems can assess detected positions and movement to flag potentially dangerous interactions.
However, distance estimates from ordinary cameras may be unreliable without appropriate calibration.
Physical separation, trained operators, traffic rules, and designated pedestrian routes remain essential.
5. Slip, Trip, and Fall Hazards
Computer vision may identify selected visible floor hazards or fall-related events, depending on the detection system and environmental conditions.
Potential examples include:
- Materials obstructing walkways
- Visible floor spills
- Objects left in pedestrian routes
- Certain worker fall events
Not every slipping or tripping hazard is visually detectable.
Small spills, transparent liquids, poor flooring conditions, and hidden obstacles may be difficult to recognise.
AI alerts should therefore support routine housekeeping inspections rather than replace them.
OSHA includes housekeeping and walking-surface hazards among the issues that should be addressed through regular workplace inspections [OSHA, Hazard Identification and Assessment].
6. Unsafe Material Handling and Storage
AI monitoring can help identify visible storage conditions that may obstruct movement or create workplace hazards.
Examples include:
- Materials blocking emergency exits
- Obstructed pedestrian routes
- Pallets placed in restricted areas
- Visibly unstable storage arrangements
- Items left in equipment movement zones
These hazards can affect worker movement, emergency access, and material-handling safety.
Camera-based detection may identify visible obstructions.
However, it cannot reliably determine every structural loading or stacking risk.
Safety teams must still assess storage procedures, load limits, and equipment suitability.
7. Smoke, Fire, and Visible Hazards
Specialised video analytics can identify certain visible smoke or flame patterns and flag them for investigation.
Potential applications include monitoring selected production and storage areas.
However, visibility-based detection has limitations.
- Smoke may be obscured.
- Lighting can affect recognition.
- Steam or dust may create false alerts.
- Some fires may develop without visible flames.
- Hazardous gases may be invisible.
Video-based detection must not be treated as a substitute for required fire alarms, gas detectors, or other approved protective systems.
Specialised video image smoke detection is recognised within the fire-detection field, but installation and use must follow applicable requirements [NFPA 72, 2019].
How Does AI Detect Manufacturing Hazards?
AI safety systems analyse available visual or sensor information and compare detected conditions with predefined safety rules.
A typical camera-based process includes:
- Capture: Cameras observe selected production areas.
- Recognise: Computer vision identifies relevant people, vehicles, equipment, or visible objects.
- Evaluate: The system compares observations with configured safety conditions.
- Flag: Potential violations or hazards are recorded or highlighted.
- Verify: Safety personnel review the findings.
- Respond: Appropriate corrective action is taken.
Detection accuracy varies by environment and use case.
A poorly positioned camera may miss unsafe activity. Obstructions, changing lighting, and crowded production areas can also affect results.
An AI-generated alert should therefore be treated as information requiring appropriate assessment, not automatic confirmation of a safety incident.
How Can Plants Identify Recurring Safety Problems?
Repeated safety observations can reveal locations, operating activities, or procedures that require stronger preventive controls.
For example:
- Frequent restricted-zone entry may indicate ineffective access controls.
- Repeated forklift proximity events may reveal traffic-management problems.
- Recurring PPE violations may indicate task-specific compliance gaps.
- Frequent blocked walkways may suggest poor material-storage practices.
The value comes from investigating why these problems continue.
Identifying repeating safety risks across plant shifts helps safety teams recognise hazards that persist across different working periods, locations, and operating conditions.
Historical investigations also provide useful context.
Treating safety incidents as early warning signals helps manufacturers connect earlier events with current hazardous conditions and investigate risks before similar incidents occur.
How Does Industry 4.0 Connect Safety Data?
Connected manufacturing intelligence helps safety teams review available hazard information alongside production activity, equipment conditions, and plant operations.
Safety records and operational information often exist across separate systems.
This can make investigations more difficult when a hazardous condition is linked to equipment operation or production activity.
Manufacturing companies can use Insightvillee as an AI Industry 4.0 platform to connect existing ERP, MES, SCADA, PLC, sensor, and plant data into one intelligent system.
This connectivity can provide operational context for:
- Equipment operating status
- Maintenance activities
- Production conditions
- Shift information
- Available safety and compliance records
Where compatible detection information is integrated, it may contribute to broader safety investigations.
However, connected plant data does not automatically establish native computer vision, PPE recognition, or camera-based hazard detection capabilities.
How Does Insightvillee Support Plant Safety?
Insightvillee connects manufacturing operations with safety and compliance information to support better plant-wide operational visibility.
As an AI-driven Industry 4.0 platform, Insightvillee gives manufacturing leaders real-time visibility across machines, production lines, and multiple plants.
Its established capabilities include:
- Safety and compliance automation
- OEE monitoring and improvement
- Predictive maintenance
- Multi-plant intelligence
- Smart production planning
This supports a connected understanding of manufacturing operations and available safety information.
Specific camera-based detection capabilities should be verified before they are presented as native Insightvillee features.
Insightvillee’s Safety and Compliance capability connects safety-related information with broader manufacturing operations, helping plant teams understand operational conditions and support compliance activities.
How Can Plants Act on AI Safety Alerts?
AI hazard detection becomes valuable when identified risks are verified, prioritised, and addressed through effective safety controls.
A practical response process includes:
| Step | Recommended action |
| Detect | Identify potential hazards |
| Verify | Confirm the observed condition |
| Assess | Evaluate exposure and severity |
| Prioritise | Address the most serious risks |
| Correct | Improve physical or procedural controls |
| Review | Check whether the hazard remains controlled |
Corrective actions may involve:
- Improving machine guarding
- Separating pedestrians and vehicles
- Strengthening restricted-area access
- Correcting unsafe storage conditions
- Improving housekeeping
- Reviewing worker safety procedures
OSHA recommends prioritising hazards according to potential severity, likelihood, and worker exposure [OSHA, Hazard Identification and Assessment].
Safety requirements also vary across manufacturing industries.
The relevance of AI applications across manufacturing industries depends on the hazards present in each sector, the available monitoring infrastructure, and the suitability of specific detection methods.
Where Should Manufacturers Apply AI Safety Monitoring?
Manufacturers should prioritise AI safety applications according to the hazards present, the quality of available data, and the effectiveness of existing controls.
A practical evaluation should ask:
- Is the hazard visible or measurable?
- Can suitable cameras or sensors capture it?
- Can the system distinguish unsafe conditions reliably?
- Will an alert reach the responsible safety team?
- Are established physical safeguards already in place?
- Can corrective action be verified?
AI is most useful when the detection method matches a clearly defined safety problem.
It should support, not replace, worker reporting, inspections, equipment safeguards, emergency systems, or human judgement.